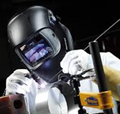
This is what I've been aiming for - welding an aluminium alloy motorcycle frame. This is the reason I started TIG welding.
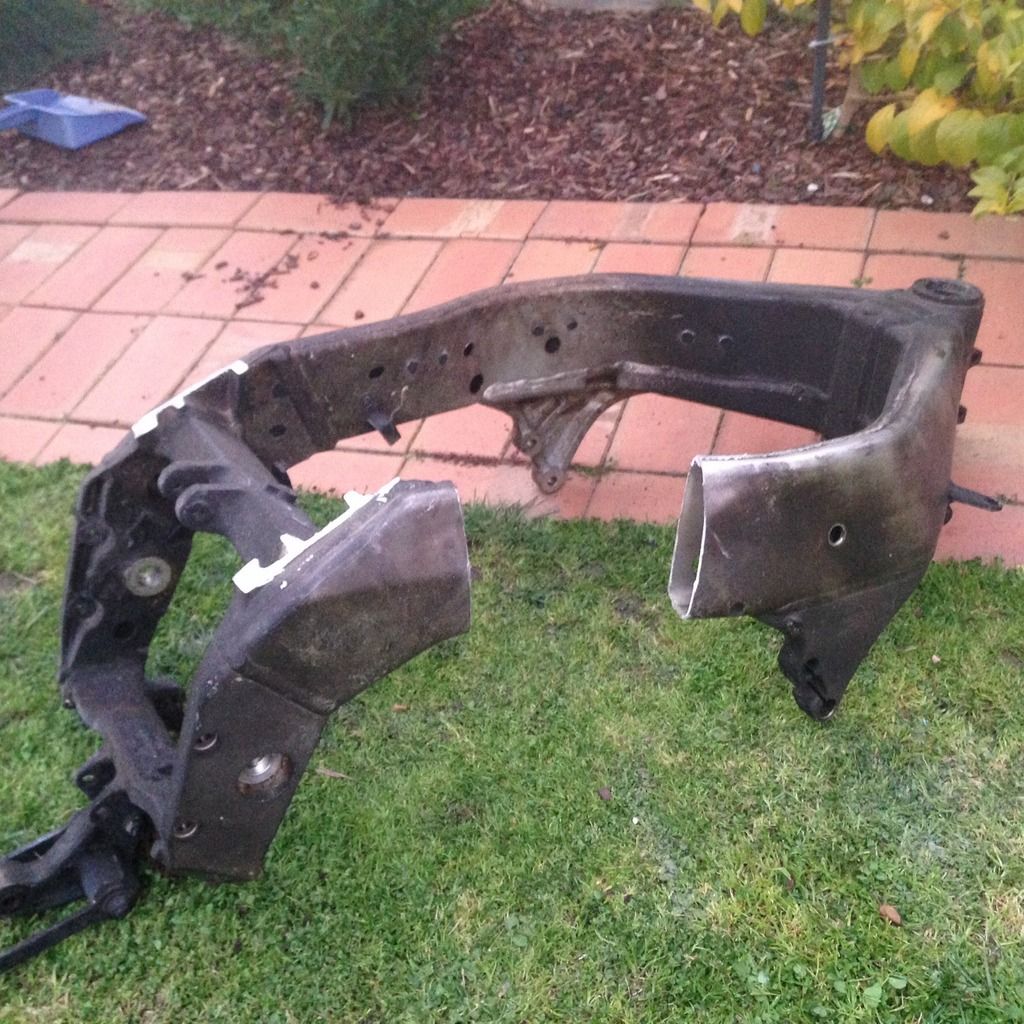
Finally got my hands on a 'donor' frame (long story) and chopped a chunk out of it;
I don't know anything about the aluminium composition other than...it's aluminium. Ahem. Cleaned the section with a abrasive wheel and a good dose of acetone. I know, I know, could have been cleaner. Set about tacking it. Amps were 100, using 1.6mm zirconiated electrode and 2.4mm filler rods of 5356. Thought the amps felt a bit high as I tacked - had a puddle in almost no time.
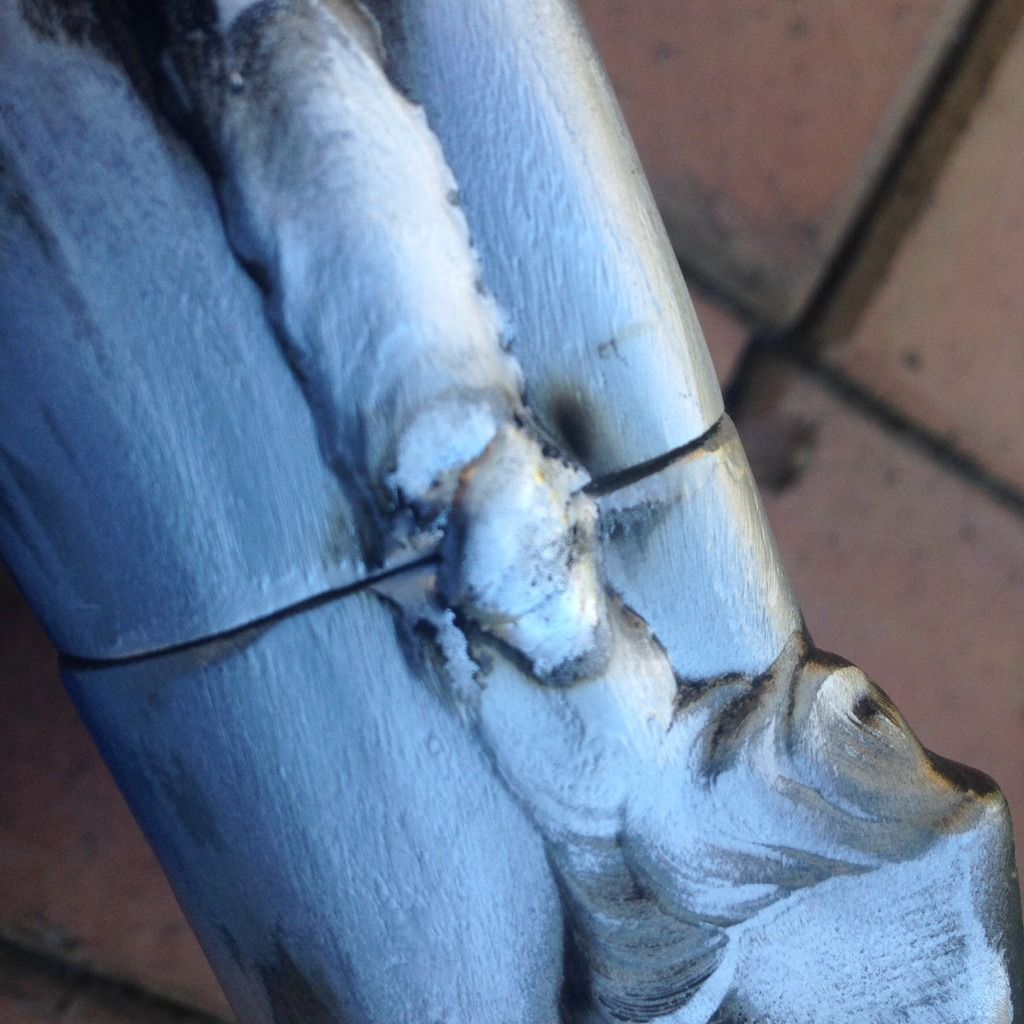
I then backed off to 85 amps for the main weld as the tack area had been pretty thick yet melted fast. The main alloy bead is about 2.4mm thick. Lit up on it and it melted fast. Used a 'laywire' kinda style with the rod. Bead seemed kinda ropey to me, think I may have been staying too cold after I lit up for fear of melt through.
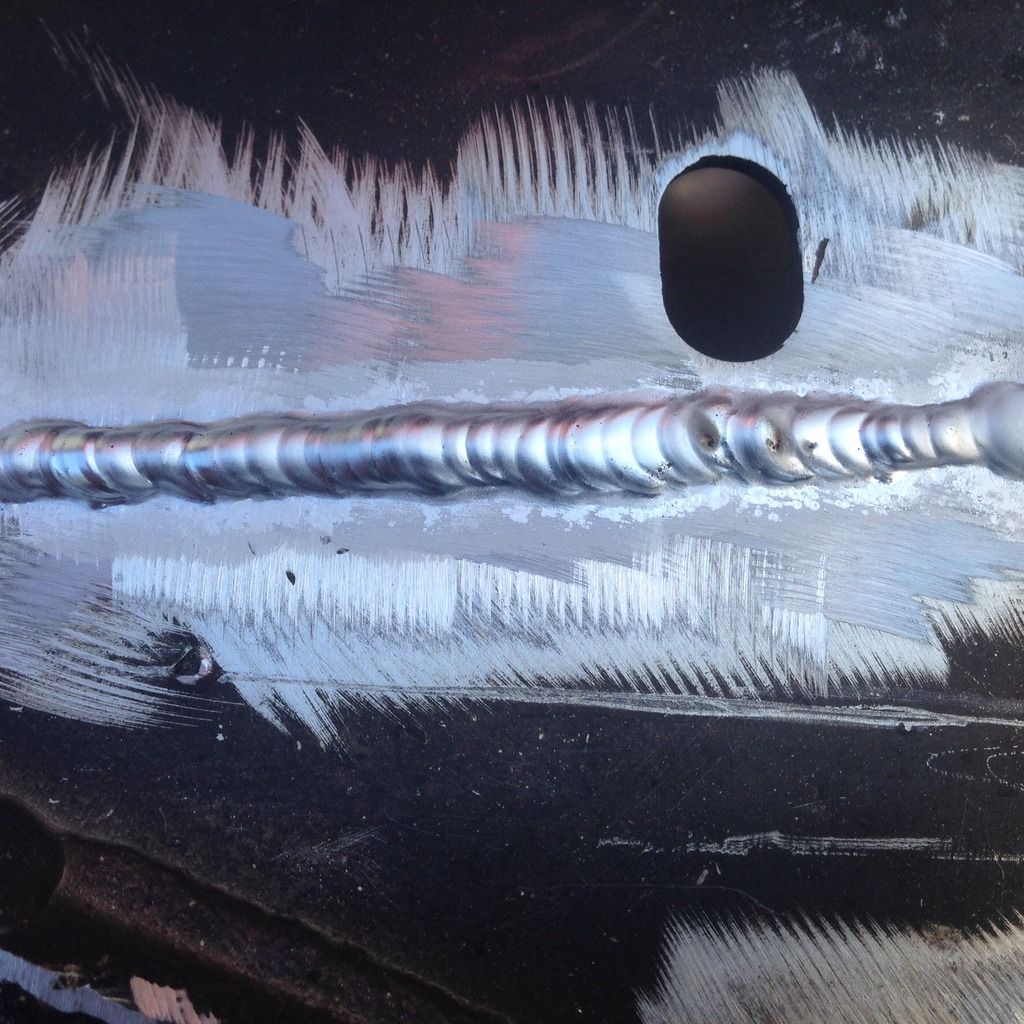
Then I flipped the beam over, only to find that a thin gap (1mm?) had, of course, opened up on the other side as I had only 'edge tacked' the beam. Newbie mistake! Lit up on it hoping to successfully fill the gap. Holy cow did that gap swallow some filler!
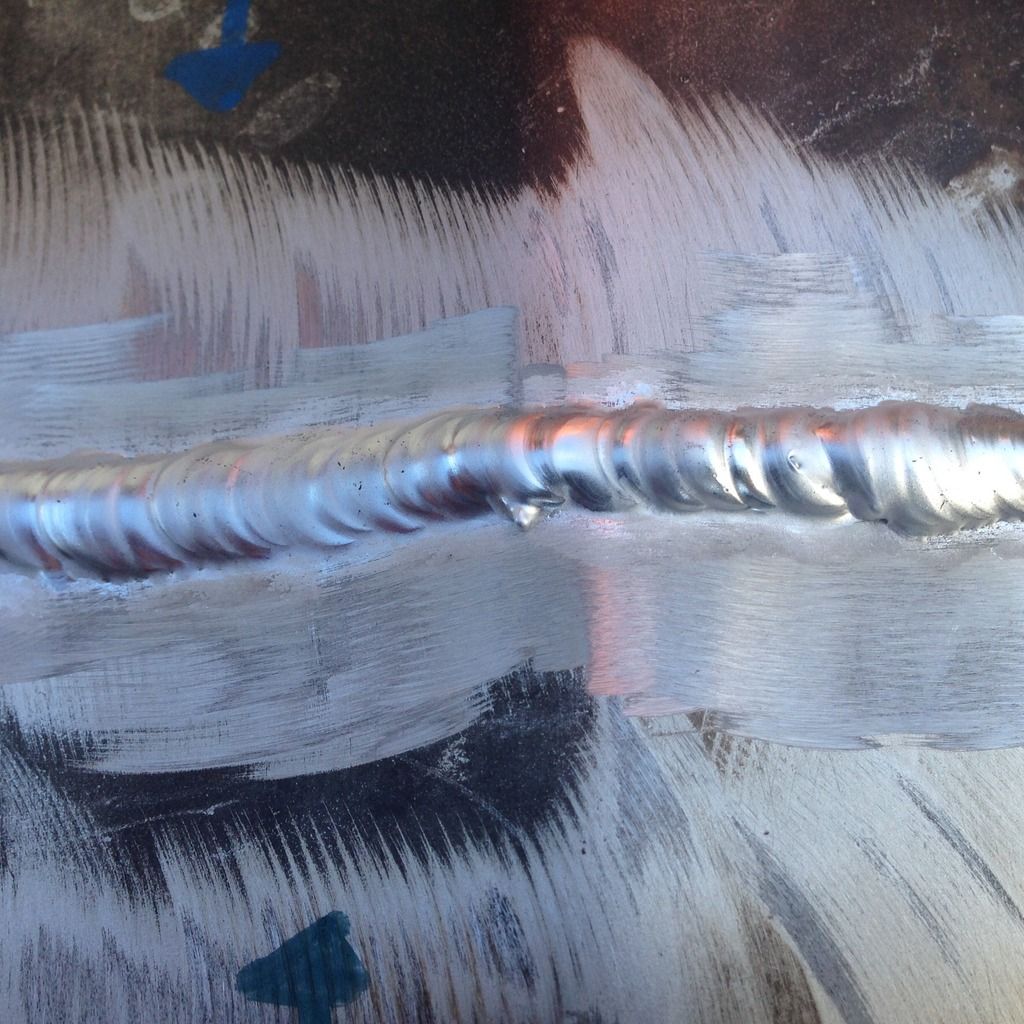
And that's the result. My feelings are that the weld isn't as tidy as it could be and on one side definitely too cold. I can see light peppering in the weld here and there - should have cleaned better. And I need to practise my filler feed hand for when things are moving fast.
Have to say I was a bit surprised at how quickly I got a puddle going, Miller guide online recommended more amps (the way I understand it.)
Sorry to be the forum pest and keep flooding you guys with this stuff, but you are my mentors and I am very eager to learn. The good news is...I have a whole frame to practise on!
Kym